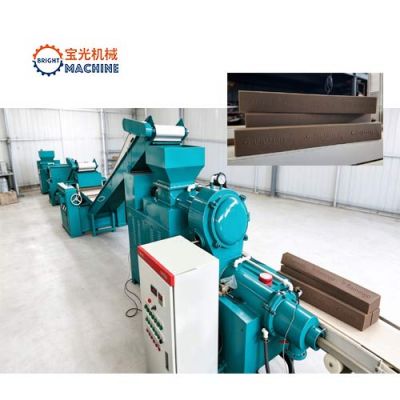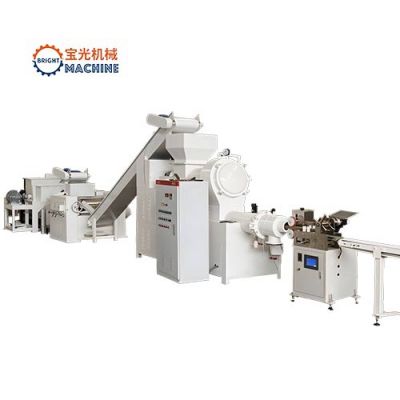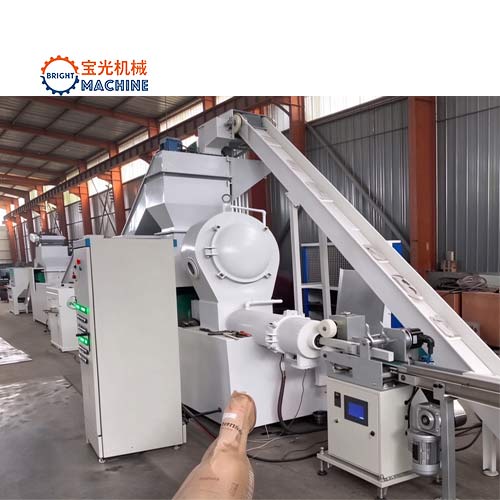
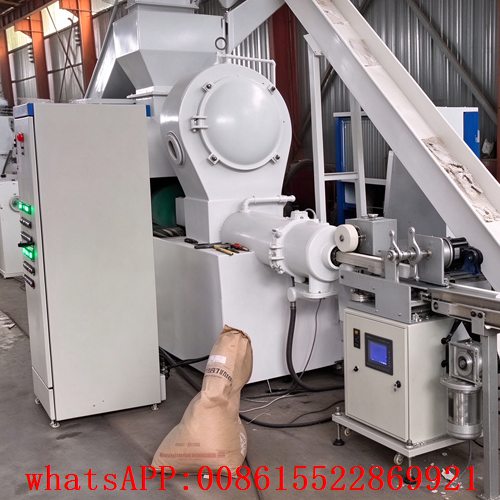
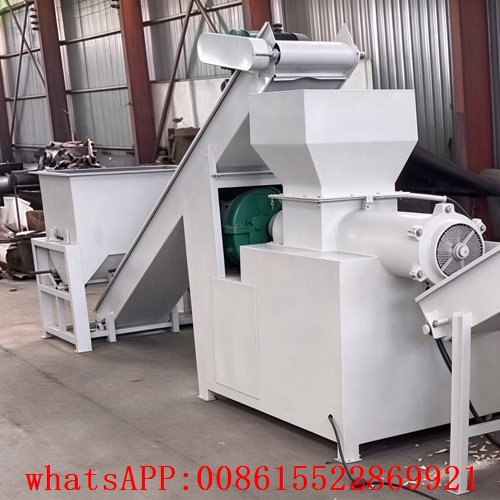
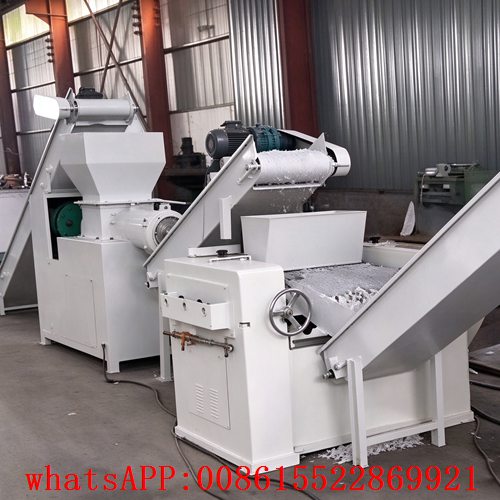
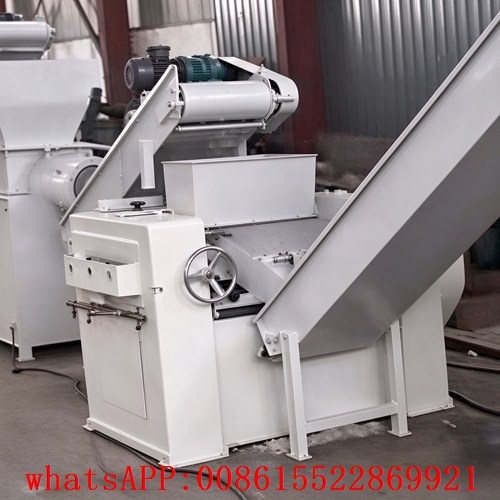
High-Torque Twin-Z Blade Soap Mixer (Shear Blending Unit)
Mechanical Structure: Heavy-duty reinforced mixing trough constructed from AISI 304/316 stainless steel with dual counter-rotating Z-shaped agitator blades.
Drive & Torque: High-torque helical gear reducer driven by a heavy-duty motor, engineered to process high-viscosity soap noodles and additives efficiently.
Process Function: Delivers intensive mechanical shear to homogenize soap noodles, colorants, liquid fragrances, titanium dioxide, and active ingredients without dead zones.
Discharge System: Pneumatically controlled bottom discharge gate ensuring quick cycle times and zero residue carryover between batches.
Fine Soap Refiner / Duplex Refining Plodder (Particle Homogenization)
Filter Grid & Mesh: Fitted with a high-strength perforated refining plate (hole diameter: 0.8–1.5 mm) backed by a stainless steel screen filter to trap un-saponified grit and particles.
Thermal Control: Integrated jacketed barrel with multi-zone heating/cooling channels allowing precise temperature management to maintain optimal mass plasticity.
Auger & Barrel: Screw augers manufactured from special wear-resistant alloy/stainless steel with variable-pitch geometry to minimize shear heat buildup.
High-Precision Three-Roll Mill (Micro-Refining & Flaking)
Roll Material & Hardness: Three horizontally arranged chilled cast alloy rollers (surface hardness: HRC 60–65) ground with dynamic crowning to withstand deflection under intense hydraulic compression.
Speed Ratio: Differential rotational speeds across the fast, medium, and slow rolls (typically 1:2.5:6 ratio) generate extreme friction and shear stress.
Micron-Level Clearance: Hydraulic or manual micrometer gap control allows precision roll adjustment down to 0.02–0.05 mm, crushing crystalline structures into micro-thin flakes for a velvety soap texture.
Vacuum Duplex Plodder / Extruder (Deaeration & Continuous Bar Formation)
Two-Stage Extrusion: Upper stage acts as a vacuum feeder and cutter; lower stage acts as the primary compression extruder.
Deaeration Performance: Liquid-ring vacuum pump system achieves a continuous negative pressure up to -0.092 to -0.098 MPa, eliminating micro-air pockets, pinholes, and internal voids to prevent soap cracking.
Temperature-Controlled Extrusion Head: Multi-zone PID-controlled circulating water jacket on the extrusion cone ensures smooth surface melting, precise die head pressure, and high-gloss bar finish.
Servo-Synchronized Flying Cutter & Stamper (Precision Cutting Unit)
Kinematic Synchronization: Servo-motor driven rotary or guillotine cutter linked directly via encoder feedback to the plodder’s linear extrusion speed, delivering cutting precision within ±0.5g per bar.
Die Mechanism: Pneumatic or hydraulic stamping press with quick-change aluminum/brass mold cavities, equipped with internal chilled fluid channels to prevent soap sticking during high-speed logo impression.
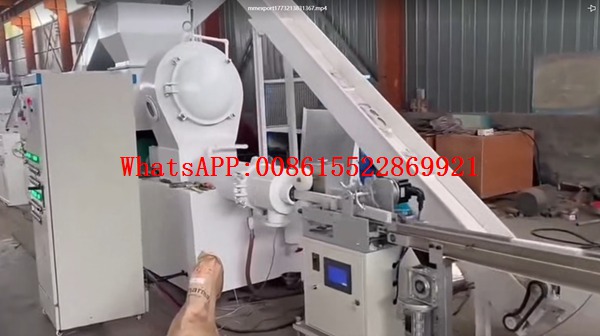
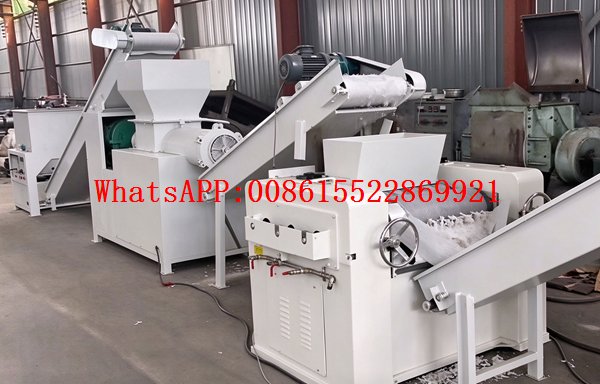
Production Capacity: 1000 kg/h nominal throughput (expandable up to 1200 kg/h depending on soap formulation and moisture content).
PLC Automation & Control: Siemens/Schneider PLC architecture with a multi-language HMI touchscreen panel, featuring real-time monitoring of motor current, barrel pressure, vacuum levels, and zone temperatures.
Material Integrity: All contact parts (hopper, augers, rolls, cutter blades, dies) are fabricated from SUS304/SUS316, conforming to international GMP standards.
Energy Optimization: Equipped with Variable Frequency Drives (VFD) on all major motors, lowering startup current peak loads and reducing overall energy consumption by up to 20-25%.
Safety Features: Complete emergency interlocks, safety guards on rotating rolls, pressure relief valves, and overload protection compliant with CE machinery safety directives.
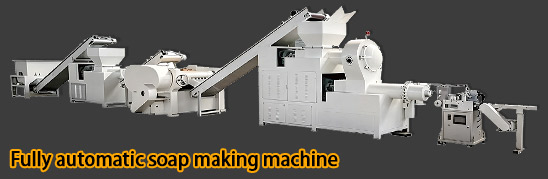
Tianjin Bright Machinery Equipment Co., Ltd. is a leading manufacturer specializing in automatic soap-making machinery and pharmaceutical packaging equipment. With nearly two decades of expertise, our high-performance solutions range from soap processing lines (toilet and laundry soap) to capsule fillers, tablet presses, blister packing, and cartoning machines, widely serving the personal care, food, and pharmaceutical industries.Certified with ISO9001 and CE standards, we ensure premium quality, innovative technology, and full compliance with strict global standards. Driven by our philosophy—"Not the best, but better"—we offer tailor-made automation solutions, complete technical support, and dedicated after-sales services to clients across more than 100 countries worldwide.
Contact Person:Jenna Liu
Tel/WhatsApp:8615522869921
E-mail:emily@tjbrightmachine.com
Add: Yinzuo Building, No. 35, Second Avenue, Tianjin TEDA